Case study
Aerospace traceability on curved components
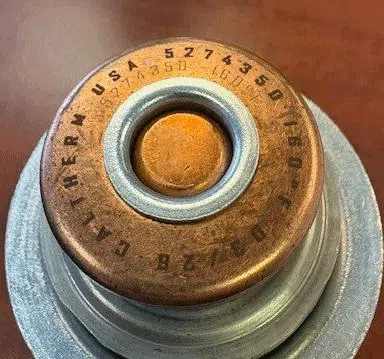
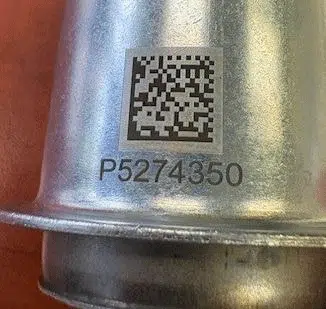
Permanent, legible marking of small cylindrical valve bodies, guaranteeing both internal and external traceability within an aerospace manufacturing environment.
30W fibre laser sized for a 5-second cycle
A 30W source was chosen so that the 5-second-per-part cycle could be met on stainless steel, brass and copper components alike.
Standard rotary-axis configuration, no bespoke engineering
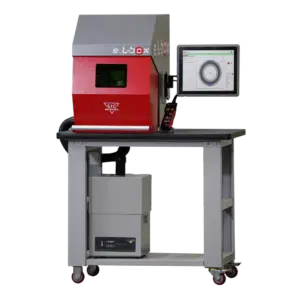
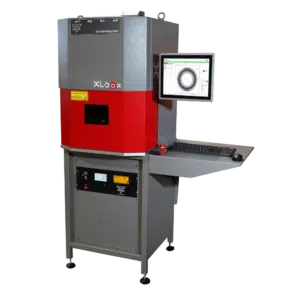
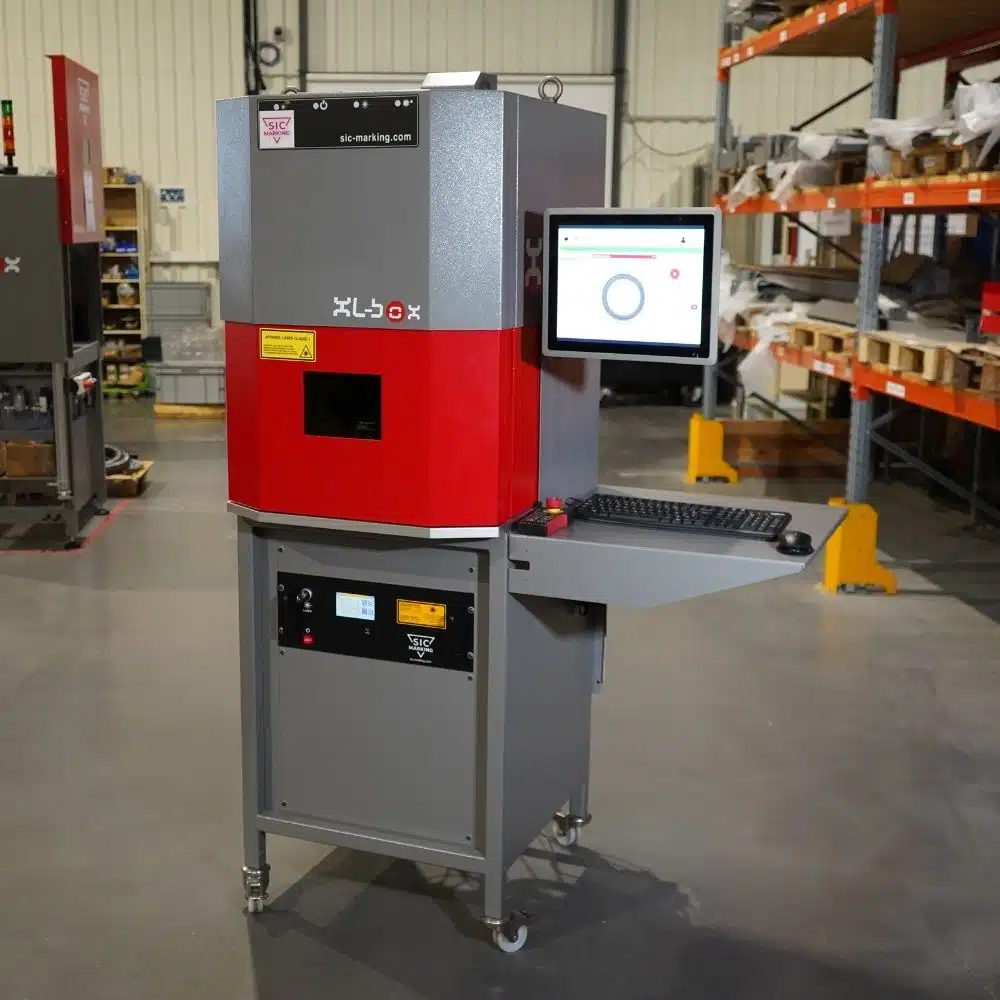
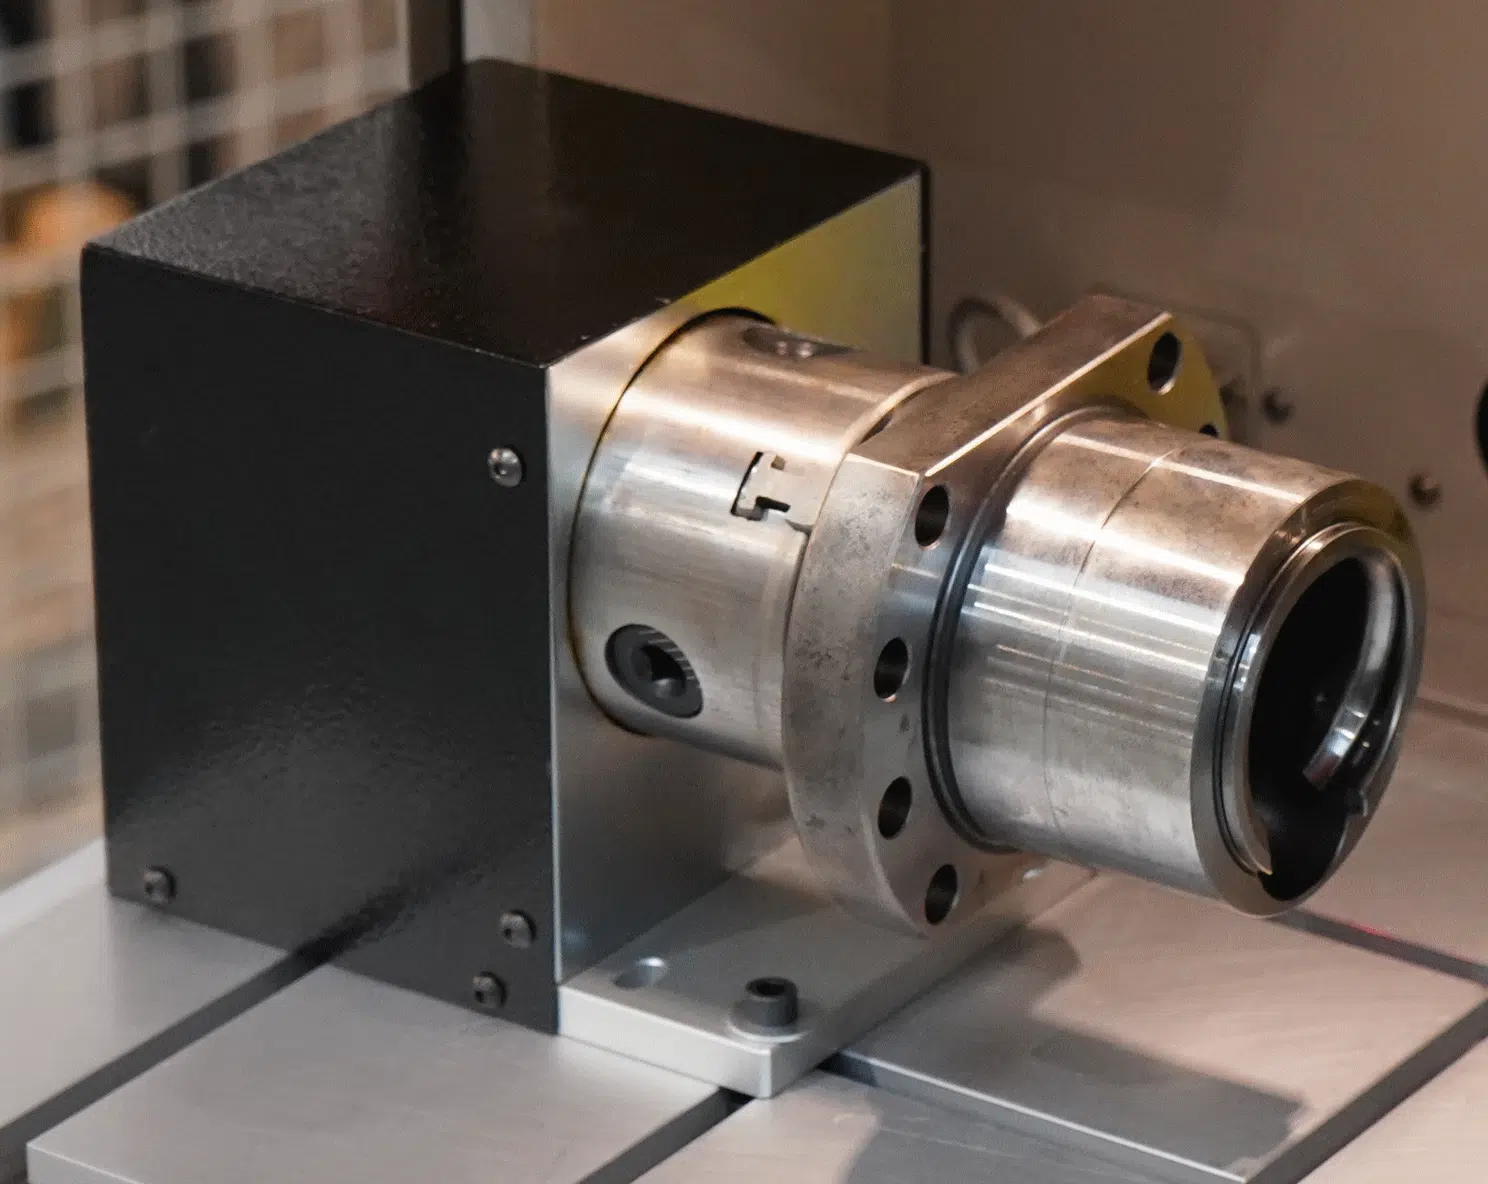
Fitted with a rotary axis, the XL Box EASY marks the entire circumference of round workpieces using a standard configuration: chassis, 254 mm lens and fume extraction.
Cycle time and marking quality
A 5-second cycle time was reached from the very first production runs, with marking quality to specification on all three materials.
The customer produces thermostatic pressure-regulating valves fitted to aerospace thermal management systems. Every valve body must carry a permanent, legible mark comprising the serial number, the staging number and the company name. This marking underpins both internal production traceability and external identification over the whole service life of the component, including the ability to trace any manufacturing defect back to a specific production batch.
The existing marking method was unable to keep up with the throughput demanded. Production is organised over three shifts, each run by a single operator, within a clean manufacturing area. Whichever marking solution was adopted had to produce consistent results at 5 seconds per part without making the operator’s routine any more complicated.
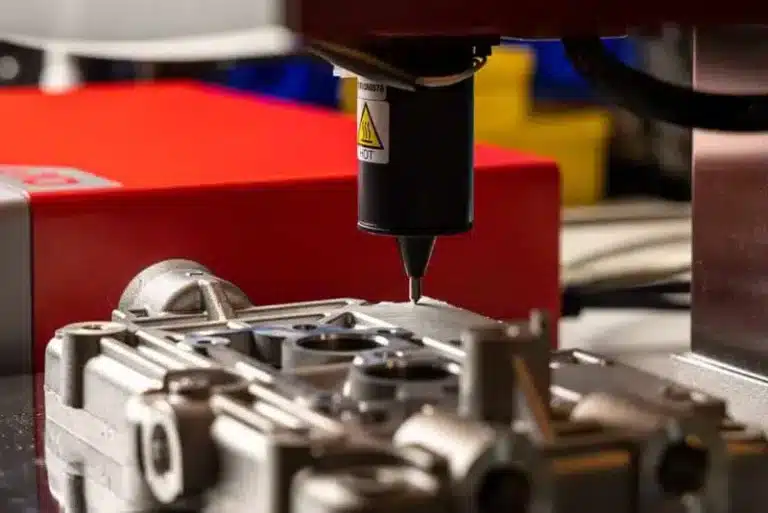
The main obstacle was geometric: valve bodies are small, round components with a curved outer surface. Producing a clean, legible mark on a cylindrical surface at pace, on finished stainless steel, whilst also processing brass and copper components on the same line, called for a solution capable of coping with both the curvature and the range of materials without compromising quality or cycle time.
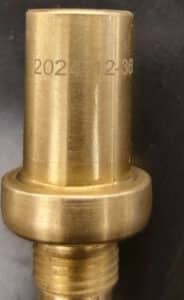
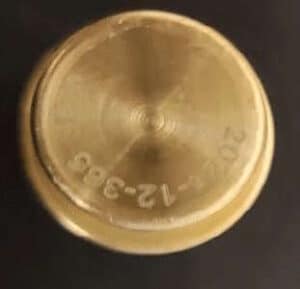
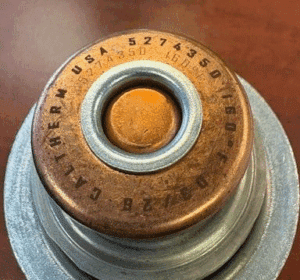
The valve bodies are small cylindrical components. Marking a curved surface with a flat-field laser set-up causes the focal point to drift as the geometry curves away from the lens, which results in uneven or illegible characters. On a part of this kind, a rotary axis is essential in order to mark its entire surface.
Three materials pass through the production line: stainless steel, brass and copper. As each one absorbs laser energy differently, SIC MARKING had to establish and supply marking parameters tailored to every material, so that marking quality remains consistent across the complete range of parts.
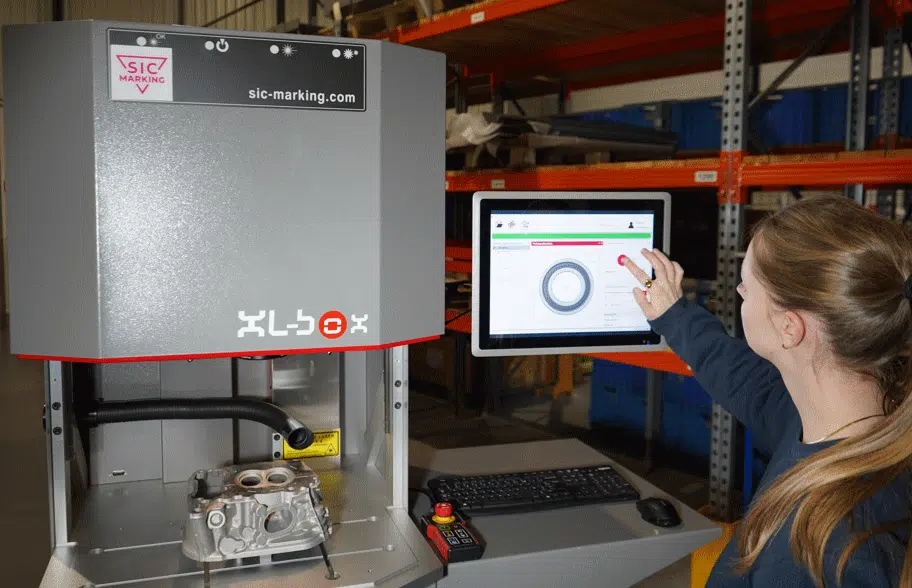
The operation is carried out manually, by one operator per shift over three shifts. The set-up therefore had to be simple enough to deliver repeatable results whoever is at the station.
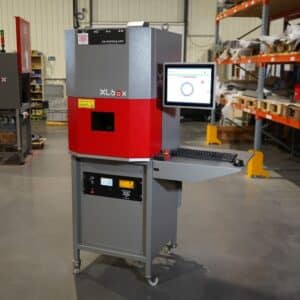
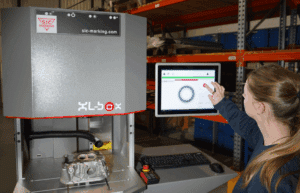
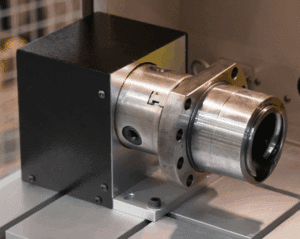
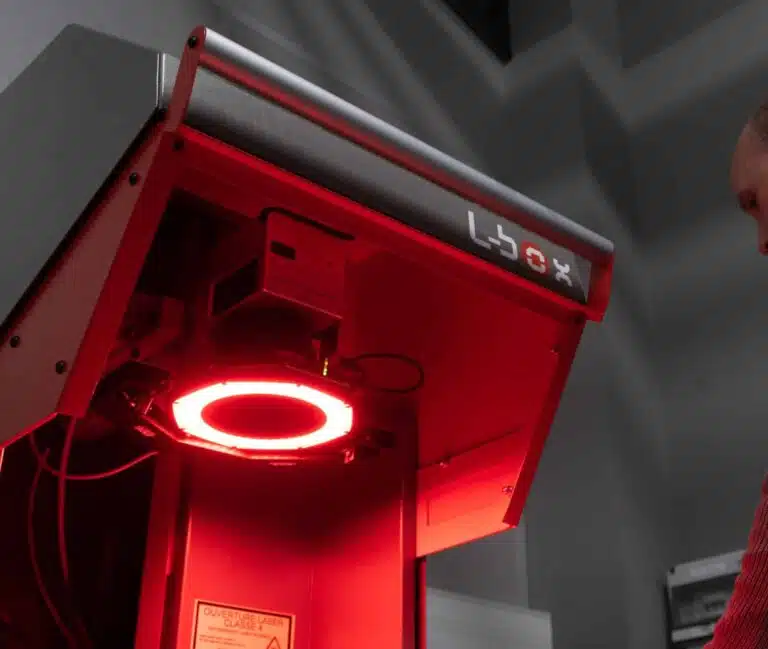
SIC MARKING proposed the XL Box EASY fitted with a 30W fibre laser source, paired with a rotary axis, a dedicated chassis fixture and a lens with a 254 mm focal length. A Fumex extraction unit was built in to preserve air quality within the clean production area.
The 30W source was chosen precisely to satisfy the 5-second cycle time requirement.
Thanks to the rotary axis, the system can mark right around the circumference of the valve body.
The 254 mm lens offers a marking field matched to the small dimensions of the part and to the character height needed for legible alphanumeric content. The whole configuration is standard equipment drawn from SIC MARKING’s existing product range and adapted to the customer’s fixturing requirements, with no bespoke engineering involved.
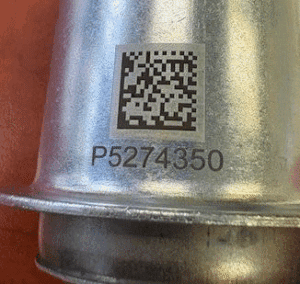
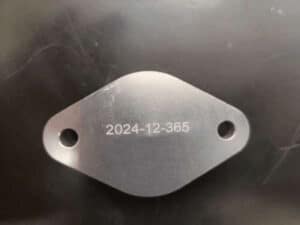
The target cycle time of 5 seconds per part was reached from the first production runs. Marking quality satisfied the legibility requirements for serial numbers, staging numbers and company identification, on stainless steel valve bodies and on brass and copper components alike.
SIC MARKING supplied the marking files together with laser parameters adapted to each material, allowing the customer to go into production with a validated set-up instead of spending time developing parameters themselves.
Every part now bears a permanent identification supporting both in-house tracking of manufacturing defects and external traceability across the whole product life cycle. Run manually over three shifts, the standard configuration gives repeatable results with no operator-dependent adjustment. Sample marking reports and photographs of parts recorded during qualification confirmed that marking quality and production rate comply with the defined specifications.
Our solutions
Discover our products
Discover our flagship laser, dot peen and scribing equipment, from portable markers and in-line integrable modules to standalone marking stations.
Would you like to know more?
Get in touch!